Choosing among the Top Antique Metal Casters for Global Buyers requires more than attractive photographs. Buyers must examine alloy composition, workshop experience, casting methods, restoration records, and export documentation. A convincing bronze finish cannot hide weak details, porous surfaces, or uncertain provenance.
The global metal casting industry provides useful context. Grand View Research valued the market at approximately USD 151.4 billion in 2023 and projected continued growth through 2030. However, antique and reproduction casting remains a smaller, less transparent segment. Public reports rarely separate heritage-style work from industrial production. That gap matters. Comparisons should therefore combine market evidence with direct supplier verification, sample inspection, and customer references.
John Campbell, a respected casting technologist and author of Complete Casting Handbook, stated, “The quality of a casting is determined by the quality of the liquid metal.” His observation remains practical. A reputable Antique Metal Casters workshop should explain its alloys, melting controls, mold materials, finishing stages, and inspection procedures. Ask for close images of edges, lettering, patina transitions, and rear surfaces. Those details reveal craftsmanship.
There is no perfect ranking. Some suppliers excel at historical replication, while others deliver stronger custom engineering or larger production volumes. That difference can confuse buyers. It deserves closer attention.
This guide evaluates leading Antique Metal Casters through transparent criteria, including technical capability, documented experience, communication quality, material consistency, and international fulfillment readiness. Buyers should still verify current certifications, shipping requirements, and product claims independently before placing an order.
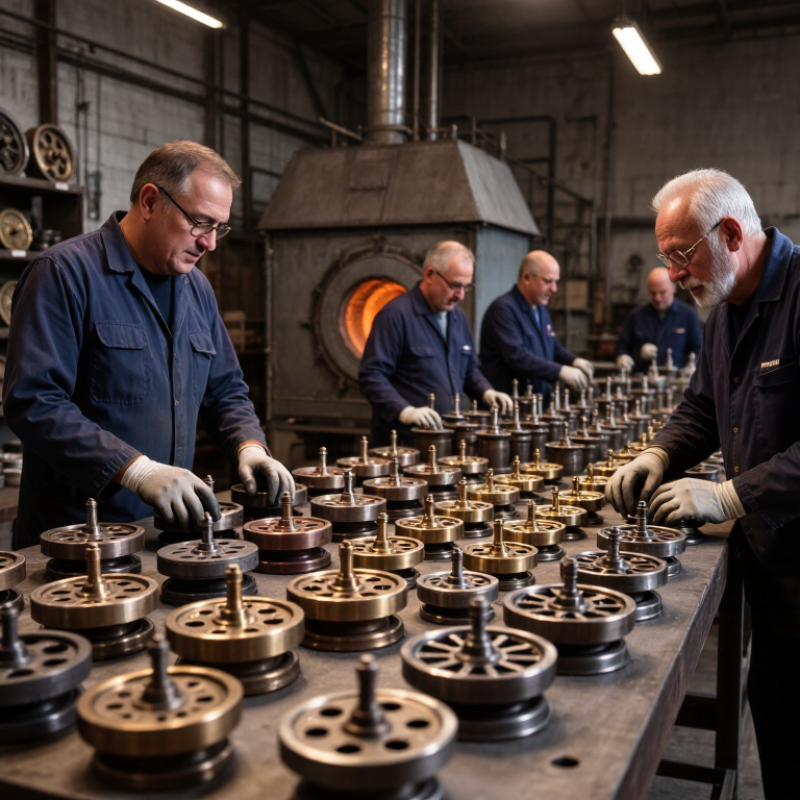
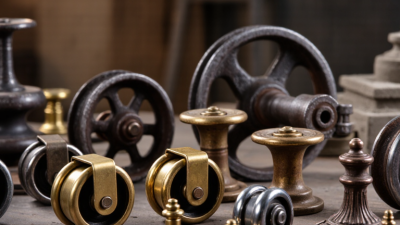
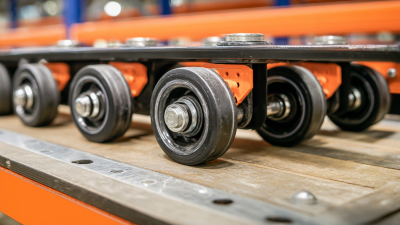
A high-quality antique metal caster combines reliable movement with convincing period character. Its frame should feel solid, not hollow or loosely assembled. Cast iron, brass, and steel each age differently, so experienced buyers examine the metal closely. A genuine aged surface often shows uneven patina, small abrasions, and softened edges from years of handling. Artificially darkened metal can look too uniform.
Function still matters. The wheel should rotate smoothly without excessive wobble, grinding, or sharp resistance. Check the axle, mounting plate, screws, and swivel joint for cracks or careless repairs. Details matter. A caster may look attractive in photographs but fail under practical use. I once inspected a decorative piece with beautiful oxidation; its axle was bent and unusable. That mistake reinforced a simple lesson: appearance cannot replace testing.
Professional sellers should provide precise measurements, material details, estimated load capacity, and clear photographs of hidden areas. Buyers should compare the wheel diameter, plate holes, overall height, and intended furniture weight before ordering. A short rolling test on a flat surface can reveal problems quickly. Packaging also reflects reliability, especially for international shipments. Each caster needs protection around its edges and moving parts. Even careful assessments have limits. Age, restoration, and previous use are sometimes difficult to confirm with certainty. Honest descriptions should identify those uncertainties instead of promising perfection.
International buyers should choose antique metal casters that combine historical accuracy with dependable export procedures. The strongest suppliers usually explain alloy composition, mold methods, surface finishing, and restoration limits. They also provide dated photographs, dimensional drawings, sample approvals, and clear reproduction labels. Provenance matters.
The World Bank’s 2023 Logistics Performance Index compares 139 economies across customs, infrastructure, tracking, and delivery reliability. These measures are practical when evaluating a caster’s international service. A capable workshop should offer export packing, commercial invoices, harmonized tariff codes, and shipment tracking. UNCTAD’s Review of Maritime Transport reports that over 80% of global merchandise trade by volume moves by sea. Therefore, corrosion protection and vibration-resistant crating are not minor details. A bronze door fitting should arrive wrapped, cushioned, and separated from abrasive materials.
Ask for test certificates when the project requires unusual alloys or structural strength. Independent material analysis can verify copper, tin, zinc, lead, or iron content. Small errors matter. An incorrect alloy may alter color, weight, and machining behavior. ISO 9001 certification can indicate controlled processes, but it does not prove historical authenticity. That distinction is often missed. Buyers should also check references from overseas restoration projects, response times, insurance terms, and procedures for damaged deliveries. No shortlist is flawless; even experienced buyers can underestimate customs delays or finish differences between approved samples and larger production pieces.
When comparing antique metal casters, begin with the alloy, not the decorative finish. Bronze offers warm color and strong detail, while cast iron feels heavier and shows a sharper, darker surface. Aluminum is lighter, but it may look too clean for older work. The 2023 World Census of Castings, published by Modern Casting, reported global casting output above 100 million tonnes in 2022. That scale shows why material knowledge matters. Mass production can imitate hand-finished textures surprisingly well.
Examine sprue marks, seams, tool traces, and uneven oxidation. Experienced casters usually leave small variations around recessed details. Perfect repetition can be a warning sign. X-ray fluorescence testing can identify surface elements, but it cannot prove an object’s age alone. Provenance, workshop records, repair history, and consistent wear remain essential. The International Aluminium Institute reports that recycled aluminum uses roughly 5% of the energy required for primary production. That figure supports material sustainability, not authenticity. I sometimes trust patina too quickly. That is a mistake. Artificial aging can appear convincing under warm gallery lighting.
Tips: Request close photographs of the underside, interior, and attachment points. Compare weight with the object’s dimensions. Ask whether testing was performed by an independent specialist. Look for written findings, not confident promises. A useful report should name the alloy, method, limitations, and examiner’s qualifications. Also inspect repairs: fresh solder, modern screws, or sharp tool marks may reveal later intervention. A second opinion is sensible, especially when the surface looks unusually perfect.
Choosing top antique metal casters for global buyers requires more than inspecting attractive photographs. Export experience, customization control, and compliance records often reveal the real supplier quality.
Experienced casters should provide clear material specifications, product dimensions, weight, and country-of-origin documents. Ask for the correct customs classification before shipment. Requirements can vary by destination, especially for products containing lead, cadmium, or restricted surface treatments. Reliable suppliers should support independent laboratory testing when needed. They should also explain packaging methods, moisture protection, and damage claims. A wooden crate may protect heavy castings better than thin foam.
Customization deserves practical questions. Can the workshop reproduce a hand-aged bronze appearance without hiding casting defects? Can it adjust wall thickness, mounting holes, lettering, or patina color? Request a sample made from the final alloy and finishing process. Digital drawings help, but they do not replace a physical sample. Small details matter.
I usually inspect edges, weld marks, thread accuracy, and surface consistency under strong light. I also compare the approved sample with packed production pieces. Mistakes happen. One overlooked tolerance can make installation impossible. That is why written approval sheets, inspection photos, and staged payments are useful safeguards. Suppliers should disclose production limits instead of promising everything. A low quotation may exclude testing, export packing, or replacement support. That is not always obvious. Reliable communication remains part of compliance, not merely good service.
Top Antique Metal Casters for Global Buyers?
How to Select the Right Antique Metal Caster for Your Project
Selecting an antique metal caster requires more than comparing prices. Start with the alloy, casting method, and intended use. Brass, bronze, iron, and aluminum each create different weight, texture, and aging effects. Ask for technical data, sample pieces, and clear details about dimensional tolerance. A decorative handle may accept minor variation. A fitted architectural part usually cannot.
Review the caster’s project experience with similar shapes and surface finishes. Request close-up photos of pores, edges, patina, and polishing marks. These details reveal more than a polished catalog image. Confirm mold-making capabilities, minimum order quantities, lead times, and packaging standards. For international shipping, require accurate material descriptions, invoices, and origin documents. Check whether the finished item meets the safety and import requirements of its destination market.
Test before committing. A small prototype can expose shrinkage, weak corners, uneven color, or unwanted brittleness. It may feel slower, but reworking a full production run costs more. Do not rely on the phrase “antique finish” alone. Define the target appearance with physical references, color samples, and acceptable variation ranges. Some natural inconsistency adds character. Too much inconsistency looks careless.
A dependable caster communicates limitations early and records changes in writing. Still, no process is perfect. Metal can react differently across batches, especially with hand-applied patina. Build inspection time into the schedule, and keep a retained sample for future comparison.
| Selection Dimension | Recommended Benchmark or Option | Why It Matters for Antique-Style Projects | Questions to Ask the Caster | Global Buyer Check |
|---|---|---|---|---|
| Casting Process | Sand casting for large, textured, or traditionally styled parts; investment casting for smaller parts requiring finer detail; permanent-mold casting for repeat production with consistent dimensions. | The process affects surface texture, dimensional repeatability, minimum wall thickness, tooling cost, and the visibility of authentic casting marks. | Which process is suitable for the part size, quantity, alloy, and required surface detail? Can sample parts be approved before production? | Request process documentation and a pre-production sample. |
| Common Antique-Style Alloys | Bronze, brass, cast iron, ductile iron, aluminum, and zinc-based alloys, selected according to strength, weight, corrosion resistance, and finishing requirements. | Alloys develop different patinas and respond differently to polishing, chemical antiquing, waxes, lacquers, and protective coatings. | What is the exact alloy designation? Is chemical composition verified for each production batch? | Ask for a material certificate and applicable test report. |
| Design Reproduction | 2D drawings, 3D CAD files, physical originals, or accurately scanned reference parts. | Antique reproductions often include irregular contours, relief details, lettering, and historical surface features that must be documented clearly. | Can the caster recreate damaged or worn details without changing the intended appearance? How will shrinkage and draft angles be handled? | Confirm ownership or permission to reproduce protected designs. |
| Dimensional Control | Use drawing-specific tolerances rather than one general tolerance for the entire part. Tight tolerances may require machining after casting. | Cast surfaces and draft angles naturally vary by process, alloy, geometry, and part size. Functional interfaces need separate control. | Which dimensions are cast-critical, and which will be machined? What inspection equipment is available? | Require a dimensional inspection report for first articles. |
| Surface Finish | Options may include as-cast texture, tumbling, shot blasting, hand polishing, brushing, wire finishing, or controlled surface distressing. | A convincing antique appearance depends on controlled variation, edge treatment, recess darkening, and consistency across a batch. | Can the surface be matched to an approved physical sample? How are high points, recesses, and edges treated? | Approve a sealed color and texture master sample. |
| Patina and Protective Coating | Chemical patina, heat patina, wax, clear lacquer, powder coating, or other specified protective systems. | Patina color can change with alloy composition, humidity, handling, ultraviolet exposure, and coating thickness. | Is the patina process repeatable? What cleaning, drying, curing, and touch-up procedures are used? | Request finish samples after accelerated or practical handling tests. |
| Structural Integrity | Review wall thickness, ribs, bosses, fillets, shrinkage risk, porosity risk, and load-bearing areas during design review. | Decorative antique castings may still be used for doors, furniture, lighting, hardware, architectural fittings, or equipment covers. | What non-destructive or destructive tests are appropriate for the intended use? Are repairs permitted? | Do not use decorative-grade castings in safety-critical applications without engineering validation. |
| Quality Inspection | Visual inspection, dimensional inspection, alloy verification, hardness testing, leak testing, or radiographic testing when justified by the application. | Inspection should focus on cracks, cold shuts, misruns, inclusions, excessive porosity, distortion, coating defects, and color variation. | Which acceptance criteria will be recorded in the inspection plan? How are nonconforming parts segregated? | Include inspection criteria in the purchase order and approved drawings. |
| Tooling and Pattern Ownership | Clarify whether the pattern, mold, core box, fixtures, and digital files are buyer-owned, caster-owned, or shared. | Tooling ownership affects future sourcing flexibility, maintenance responsibility, storage, and replacement cost. | Who pays for tooling modifications? Can tooling be released or transferred if the project changes supplier? | Use a written tooling agreement before production begins. |
| Order Quantity | Prototype or low-volume production may favor flexible sand or printed patterns; repeat orders may justify permanent tooling or dedicated fixtures. | The best process depends on the total lifetime quantity, not only the first order. | What are the minimum order quantity, repeat-order conditions, and tooling amortization terms? | Compare total landed cost over the expected project life. |
| Lead-Time Planning | Separate the schedule into design review, pattern or tooling, sample casting, finish approval, production, inspection, and international transport. | Finishing and approval cycles can take as long as or longer than the casting operation, especially for color-matched antique surfaces. | What milestones require buyer approval? Which events trigger the production lead time? | Build in time for sample revisions and customs clearance. |
| Packaging and Corrosion Protection | Use separators, edge protection, moisture control, suitable wrapping, and strong export cartons or crates matched to part weight. | Patinated or polished metal surfaces can be scratched, stained, or affected by condensation during ocean or air transport. | How are finished surfaces protected from abrasion and humidity? Are packaging tests or photographs provided? | Specify packaging, labeling, and moisture-control requirements in writing. |
| Documentation | Drawings, approved samples, material certificates, inspection reports, packing lists, commercial invoices, and origin documents as applicable. | Complete documentation supports customs clearance, quality claims, traceability, installation, and future repeat orders. | Which documents are included automatically, and which require advance request? | Confirm documentation requirements with the destination country's customs broker. |
| Sustainability and Compliance | Evaluate recycled-content claims, responsible waste handling, ventilation, chemical management, worker safety, and local legal compliance. | Metal casting and chemical finishing can involve energy use, dust, fumes, and regulated substances that require controlled management. | Can the caster provide relevant environmental, safety, and chemical-management records? | Match requirements to the buyer's market and project specification. |
| Supplier Evaluation Score | Score each candidate on process capability, sample quality, alloy control, finishing consistency, inspection, communication, delivery reliability, and total cost. | A low unit price does not compensate for inconsistent patina, poor dimensional control, rework, or delayed shipments. | Can the supplier provide comparable project samples, references, and a corrective-action process? | Use a weighted scorecard and approve the supplier after sample evaluation. |
Practical selection rule: Choose the caster that can demonstrate repeatable alloy control, approved antique finishing, documented inspection, secure export packaging, and reliable communication—not simply the lowest quoted price.